FortSolda Engenharia de Soldagem
Quality in Assembly & Welding

Quality Tools Applied to the Assembly and Welding of Tanks and Equipment

Failed tests, rework and weld repairs are expensive and delay delivery. We apply Ishikawa, Pareto, 5 Whys and 5W2H right at the assembly front to find the real cause of defects and remove it, with traceable records in the databook.

4-step method

From the defect found to the action plan carried out

The four tools work in sequence. The example below follows a real job: the field erection of an API 650 storage tank.

  1. 01Ishikawa DiagramFind the root of the problem
  2. 02Pareto ChartDecide which problems to solve first
  3. 035 WhysUnderstand what caused the problem
  4. 045W2HBuild an action plan to solve the problem
01

Ishikawa Diagram

Find the root of the problem

Also called the fishbone or cause-and-effect diagram. It sorts every possible cause of a defect into six families (6M), so the team does not jump straight to the first suspect.

When to use it on site

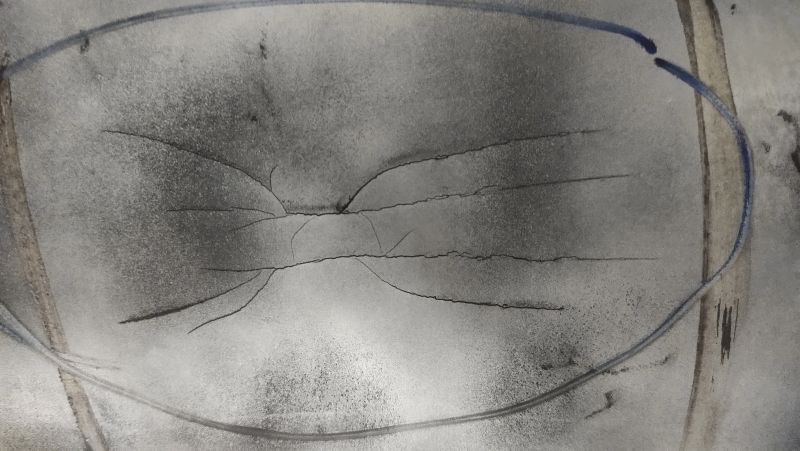
  • Recurring porosity, cracks or lack of fusion
  • Distortion and misalignment of shell plates
  • Leaks in the hydrostatic or tightness test
Applied example
Manpower

Welder not qualified (WPQ) for the vertical position

Material

Low-hydrogen electrodes left out of the oven, picking up moisture

Method

WPS parameters not followed at the work front

Machine

Loose ground clamp and power source with unstable current

Measurement

Clamp ammeter out of calibration

Environment

Wind and humidity on site with no protective screen

Porosity in the shell weld
02

Pareto Chart

Decide which problems to solve first

Ranks defects from most to least frequent and shows the cumulative percentage. A few causes usually account for most of the rejections (the 80/20 rule).

When to use it on site

  • Consolidate the job’s NDT reports (RT, UT, PT, MT and visual)
  • Choose where to invest in training and inspection first
  • Compare before and after a corrective action
Applied exampleRejected discontinuities in the tank joints100 discontinuities rejected in visual, ultrasonic and radiographic testing.
Share of each defectCumulative percentage

Porosity, lack of fusion and undercut add up to 76% of the rejections. Tackling those three causes removes most of the rework.

Pareto chart data table
DefectShareCumulative
Porosity38%38%
Lack of fusion24%62%
Undercut14%76%
Slag inclusion10%86%
Crack6%92%
Misalignment5%97%
Spatter3%100%
03

5 Whys

Understand what caused the problem

Asks "why?" in sequence until it moves past the symptom to a process cause that can be removed. It avoids fixing only the effect, such as repairing the weld without stopping the defect from coming back.

When to use it on site

  • Investigate a specific non-conformance report (NCR)
  • Dig into the most likely cause from the Ishikawa
  • Answer a complaint from the client or the inspector
Applied example

Problem: rejection for lack of fusion in the bottom joint

  1. 1Why?The weld was made with current below the WPS range
  2. 2Why?The welder set the machine by experience
  3. 3Why?The WPS work instruction was not at the work front
  4. 4Why?There is no control for distributing documents to the field
  5. 5Why?The document-control procedure does not cover field jobs

Root cause: a failure in the documentation system, not in the welder

04

5W2H

Build an action plan to solve the problem

Turns the root cause into a clear action plan: each action has an owner, deadline, place, method and cost, so it can be followed up and checked.

When to use it on site

  • Close an NCR with corrective and preventive action
  • Plan the release of a new welding front
  • Track how effective the action is in later inspections
5W2HApplied example
What
Make the laminated WPS instruction available at every welding front, with a per-pass parameter checklist
Why
Eliminate lack-of-fusion rejections caused by parameters outside the WPS
Where
Assembly fronts of tank TQ-12: bottom and first shell course
When
Before the next welded joint, within 5 working days
Who
FortSolda welding inspector, together with the erection foreman
How
Revise the document procedure, hold a 30-minute toolbox talk and measure current with a calibrated clamp meter
How Much(How much)
About R$ 800, against a repair and re-test cost per joint many times higher
Where we apply it

Quality at every stage of fabrication

Storage tanks

API 650 and NBR 7821 atmospheric tanks, from bottom and shell plates to the roof.
Pressure vessels

ASME Section VIII and NR-13 equipment, with material and welder traceability.

Industrial piping

ASME B31.3 spools and lines, with joint control by isometric.

Steel structures

AWS D1.1 structures, from walkways and supports to equipment bases.

Stages covered

  1. 1Receipt of materials and consumables
  2. 2Joint fit-up and assembly
  3. 3Welding and parameter control
  4. 4Non-destructive testing
  5. 5Hydrostatic and tightness testing
  6. 6Databook and final release
What you get

Analysis deliverables

  • Non-conformance report (NCR) with root-cause analysis
  • Ishikawa and Pareto diagrams built with your job’s data
  • 5W2H action plan with owners and deadlines
  • Effectiveness check in the following inspections
  • Records attached to the databook and available in the client portal
  • ART issued by the responsible engineer, where applicable

Does your job have defects that keep coming back?

Send us the reports or describe the problem. Our engineers will tell you where to start the analysis and which tool fits your case.